Strip deviation after roll change is rarely the fault of the new roll. The hard part is not mounting the rolls but the first coil afterwards, when the strip heads for one side, the operator trims the side guides and the crew starts asking whether the roll is bad.
Usually it is not the roll. Strip deviation after roll change traces back to the reset steps that got skipped between mounting the roll and rolling the first coil. A roll change scrambles the gap datum, the bending datum, the guide datum and the model’s learned values. Start rolling on the previous set’s habits and the datum is already wrong.
Strip deviation after roll change is unequal elongation
Strip runs to the side because the two edges are elongating differently. The side carrying more force, the side with the smaller gap or the side with higher friction pushes the strip away from itself. Everything that follows is a mechanism for creating that imbalance.
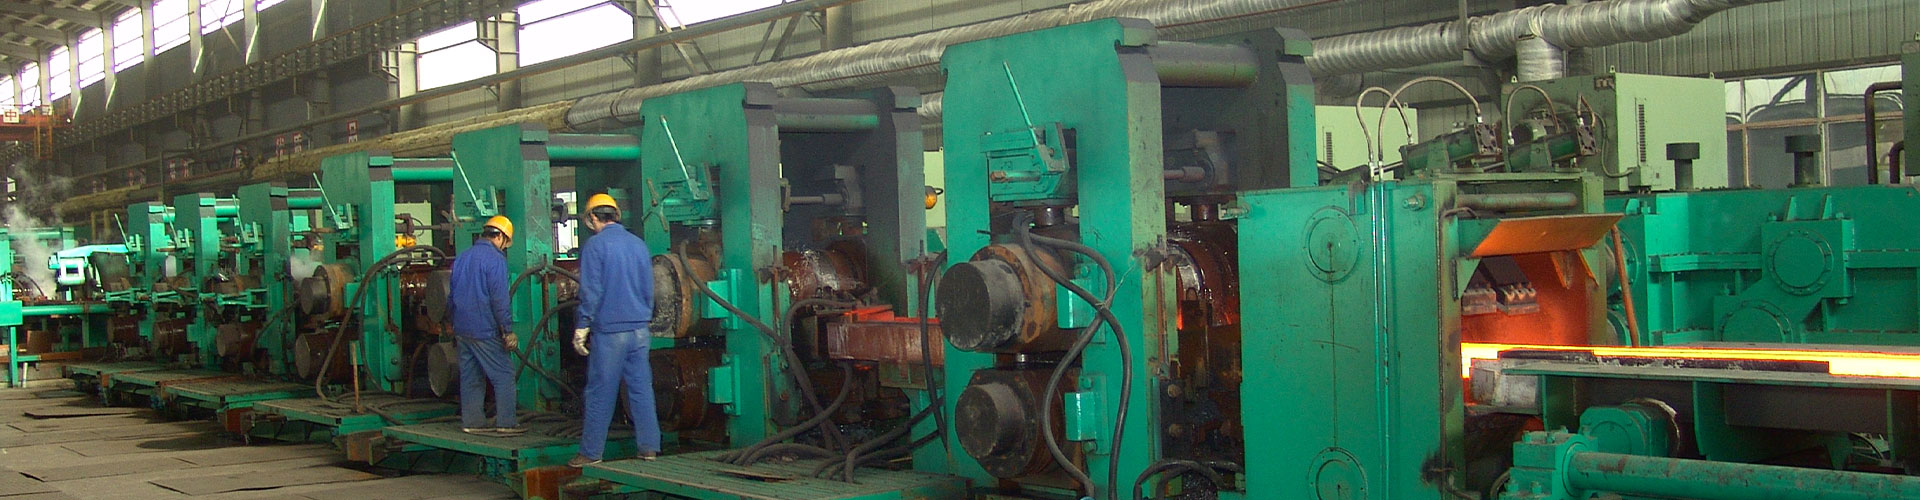
En pratique, the symptoms differ by stand. On roughing, the transfer bar leaves with an S bend or a sickle. On finishing, the strip scrapes the guide at the exit or shows a single-edge wave. The operator can pull the side guides across and recover a little, but the next coil runs the same way. Typically the first three to five coils show unstable thickness and shape, then the mill settles.
That settling pattern is the tell. A new roll that needed to bed in would not produce a repeatable direction of deviation followed by improvement. What settles is a reference that was rebuilt by trial instead of by procedure.
Gap zero and side-to-side agreement
After a roll change, the gap displayed on screen is not the gap in the mill. The old rolls came out, new diameters went in, shim stacks changed, and if the screw-down position sensor was not re-zeroed, the display can still read 8.5 mm while the real gap is out by a few tenths, or by a millimetre. This is the first place strip deviation after roll change is manufactured.
Three specific omissions cause most of it.
Zeroing the system zero without checking the two sides. When the new roll lands, does the roll face touch down on the operating and drive sides at the same moment? If one side contacts first and the other still has a gap, the gap is tilted. Roll on the displayed value and the strip naturally runs toward the loose side.
Updating the work roll diameter but not the backup roll diameter. The system uses backup diameter to calculate mill spring and gap compensation. Leave it stale and both head-end thickness and shape come out wrong.
Carrying over the previous set’s zero-adjust records. Some shops roll straight onto the old zeroing data because the new roll was never given its own calibration. The operator then applies a remembered pre-level of −0.08 and the first coil runs off. This shows up most often after finishing stand changes.
The correct sequence is short. Land the new roll, then verify both sides of the gap agree using a straight edge or a calibration routine. Enter roll diameter, backup roll diameter and profile code into the system. Build a fresh zero record for this set rather than copying the last one. And keep the zeroing force moderate, because pressing hard deflects the roll face elastically and feeds the sensor a false reading.
Bending and shifting back to zero
Many crews watch the gap during a roll change and leave bending force and roll shifting wherever they were. That habit produces strip deviation after roll change even when the gap zero is correct. The inherited value is a trap, because the last set of rolls was worn, and bending had probably been cranked up to compensate for it.
Put those same bending forces onto a fresh roll and the initial shape goes straight to a single-edge wave. The roll profile is new; the compensation is for a profile that no longer exists.
The signals are recognisable. The first coil shows centre wave or single-edge wave. Bending pressure differs noticeably between the two sides. The shift position reads off zero although nobody moved it. Or the bending cylinder has slight internal leakage, and the gap drifts slowly while holding pressure.
Bring bending back before anything else. Mount the roll, zero the gap, and only then touch bending. Return bending force to the process card’s initial value instead of inheriting the previous set. Return the shift position to zero. Compare pressure on both sides, and if the deviation exceeds tolerance, inspect the hydraulic lock and pressure reducing valve rather than forcing balance with more pressure. Bring AGC, bending and shifting to zero first, then verify at low speed.
One principle is worth stating plainly, because it is violated daily: bending controls shape, it does not correct deviation. Adding bending force to a first coil that is running off hides the reset error. It does not fix it.
AGC short-term learning and thermal growth
This is the most commonly skipped step on the floor. The AGC thickness model learns from rolling force and gap feedback, and late in the previous set’s life those learned coefficients had adapted to a worn roll. Change the rolls without clearing short-term learning, and the model keeps controlling to the old roll’s settings. Head-end thickness misses immediately, the operator starts correcting manually, and the corrections fight each other.
The action is simple: clear short-term learning after the roll change, reinitialise by steel grade and size, run the first coil at low speed while watching the head-end thickness trend, then trim the zero-offset compensation. Resisting the urge to change gains or model parameters on the first coil saves a long afternoon.
A companion issue is thermal diameter compensation. A new roll goes on cold, and over the first coils its body heats and grows, so the effective diameter is changing. Shops that apply one fixed compensation value, without separating the cold-roll stage, the warm-up stage and the steady stage, end up with a first coil that is either under- or over-compensated. Thickness and gap both drift as a result.
Guide centring
The guide is the navigation system, and one millimetre off centre sends the strip to the edge. Roll changes disturb guides more than any other component, because the guides come off, go back on, and the crossbeam bolts may not return to their original witness marks.
Three failures account for most of it, and all three surface as strip deviation after roll change. An entry guide that is off centre means the bar or strip is already skewed on the way into the groove, and it leaves more skewed. A large gap between the exit guide tongue and the roll face weakens the guidance and lets the head end scrape. Uneven clamping on a roller guide, where the roll gap was set by feel instead of with a setting bar, grips one side and releases the other, which biases the strip immediately.
After every roll change, check the guide centreline against the pass centreline. Verify the exit tongue clearance to the roll face against the process specification, which is generally no more than 0.5 mm. Set roller guide spacing with the setting bar, not by hand. Tighten crossbeam bolts diagonally and mark them. Confirm the guide base elevation aligns with the rolling line.
And do not trust the claim that nothing moved. A roll change involves disassembly and reassembly, and the baseline can shift in the process.
When the stand itself is the cause
This one is unpopular on the floor, because it means the roll change was fine and the mill was already out of alignment. Mounting a new roll simply exposes an old fault.
Three places to check.
Housing window opening. The inner faces of the window get rubbed by the bearing chock and abraded by mill scale, so the dimension grows over time. Once the clearance on one side exceeds tolerance, the chock has room to move and shifts under each rolling force pulse.
Elevation difference between sides. If the wedge blocks or chock elevations differ between drive and operating side, the roll sits skewed and the roll bodies cross. Strip then runs toward the lower side.
One-sided liner wear. During inspection, look for one liner polished and the other still intact, or a seal failing faster on one side. That asymmetry is the evidence of the shift.
The field rule is old and reliable: the wave runs toward the side carrying the force, and the bright end of the roll body is the end with the larger clearance. No amount of roll change tuning or parameter adjustment recovers this. It needs a maintenance window to measure the housing, restore the window faces and correct the elevations.
Reset sequence against strip deviation after roll change
Running this order after every roll change removes most first-coil deviation.
- Verify roll size, diameter and stand number.
- Check chock bore, shoulder and seal seats.
- Mount the roll, land it, zero the gap, confirm operating side and drive side agree.
- Enter work roll and backup roll diameters into the system.
- Clear AGC short-term learning and reinitialise by size.
- Return bending force to its initial value and the shift position to zero, then compare side pressures.
- Centre the guides, and set roller guide spacing with the bar.
- Re-check side guide and vertical roll centring.
- Run the first coil at low speed, with no full speed and no full reduction.
- Read head-end shape and deviation direction, and adjust only the zero-offset compensation, not the gains.
- Hold steady for at least 30 seconds before raising speed.
- Record gap zero, bending initial value, guide centring deviation and first-coil state in the roll change log.
Use the log
Most shops record which roll went in and what time the job finished. That is not enough to diagnose the next event, and it leaves the crew relying on memory.
Add six lines to the log: gap zero values for both sides, initial bending pressure for both sides, shift position, guide centring deviation, first-coil deviation direction, and whether learning was cleared.
When the same stand deviates to the same side on two consecutive changes, the log will usually show whether the guide was mounted off centre or the housing clearance is large. That turns a recurring argument into a measurement.
A roll change is not swapping old rolls for new ones. Plutôt, it rebuilds the datum. Skip that rebuild and the strip deviation after roll change is built in before the first coil, and even a perfect roll will run off centre.