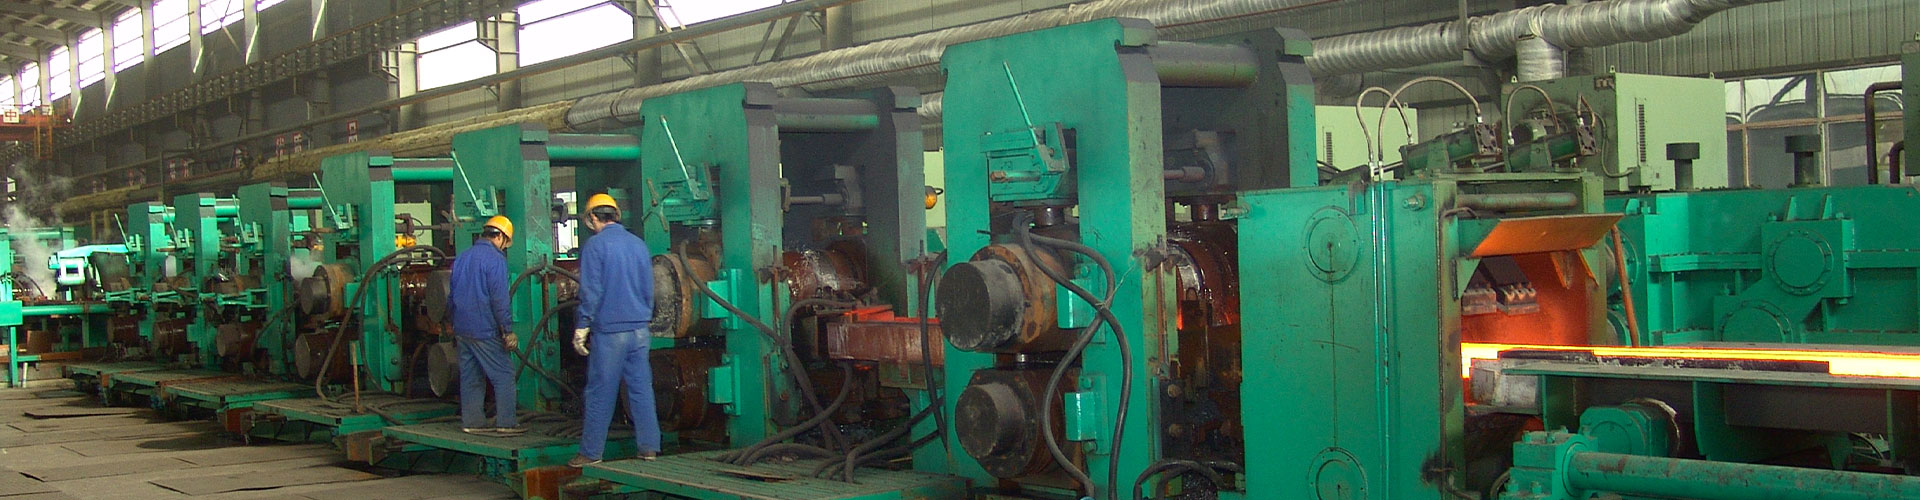
Produits laminés à froid haut de gamme tels que les tôles électroménagers, les tôles automobiles et l'acier électrique nécessitent une qualité de forme de bande extrêmement stricte. Donc, le contrôle de la forme des bandes est devenu une technologie essentielle dans l'optimisation des processus de laminage à froid, recherche d'équipement et contrôle intelligent. Les méthodes traditionnelles d'ajustement de forme incluent le pliage symétrique., roll tilting and segmented cooling. Cependant, these methods have obvious limitations when handling asymmetric strip defects. Par conséquent, the development and application of asymmetric work roll bending control provides an effective solution for common asymmetric shape problems in cold rolling production.
## 1. Current Situation and Limitations of Traditional Strip Shape Control
### 1.1 Hazards of Asymmetric Strip Defects
In cold rolling production, many factors cause uneven strip deformation. Par exemple, uneven incoming thickness, inconsistent material properties and asymmetric equipment operation on both sides of the mill easily lead to single-edge wave defects. These typical asymmetric problems reduce material yield, increase production costs and weaken product competitiveness. In severe cases, defects may also cause roll surface peeling and equipment failure.
Symmetric defects such as center waves and double-edge waves can be well eliminated by conventional symmetric bending. En revanche, asymmetric single-edge waves cannot be corrected accurately with traditional methods, and they have long restricted the improvement of cold strip quality.
### 1.2 Shortcomings of Traditional Shape Adjustment Methods
Modern cold rolling mills mainly rely on roll tilting, symmetric work roll bending and segmented cooling for shape control. Symmetric bending is the most widely used and sensitive adjustment method, but it only improves symmetric secondary and quartic shape deviations. It cannot target asymmetric strip errors.
Most asymmetric correction currently depends on roll tilting and local cooling. Roll tilting has inherent disadvantages. D'abord, it causes sudden shape fluctuation and low adjustment accuracy. It cannot completely eliminate asymmetric defects and may even induce new shape problems or strip breakage. En outre, the position closed loop and rolling force closed loop produce coupling interference during small tilting adjustments. This issue leads to poor system stability and large static errors.
## 2. Principle and System Structure of Asymmetric Work Roll Bending Control
### 2.1 Core Control Principle
Le cintrage des rouleaux de travail modifie la déflexion des rouleaux grâce à la poussée hydraulique aux extrémités des rouleaux. Il remodèle l'espace entre les rouleaux et ajuste l'épaisseur de sortie de la bande et la répartition de la tension transversale pour réaliser un contrôle de forme..
La flexion symétrique traditionnelle applique une force de flexion égale du côté entraînement et du côté fonctionnement.. La déformation du rouleau est symétrique le long de la ligne médiane du roulement, donc l'ajustement d'un seul côté affecte inévitablement le côté opposé. D'autre part, Le contrôle asymétrique du pliage des rouleaux de travail brise la limite de force égale. Il applique différentes forces de flexion des deux côtés du rouleau de travail pour produire une déflexion asymétrique du rouleau.. Cette méthode modifie la répartition de la pression entre les rouleaux et forme un espace asymétrique entre les rouleaux., qui compense efficacement l'écart d'épaisseur de coin et les défauts d'onde sur un seul bord.
### 2.2 Transformation du système de contrôle
Traditional cold rolling mills adopt synchronous control for work roll bending. Entre-temps, asymmetric work roll bending control upgrades the original system by installing independent control loops for the drive side and operation side.
The improved system supports two working modes. It maintains equal bending force for conventional symmetric shape correction, and it also allows independent force setting to achieve asymmetric adjustment. Dans l'ensemble, this transformation increases shape control freedom at low cost without replacing high-end rolling equipment.
## 3. Theoretical Analysis and Calculation Methods
To accurately analyze the performance of asymmetric work roll bending control, industry researchers have established a complete shape control model. This model covers roll elastic deformation, strip plastic deformation and strip buckling. Mature numerical calculation methods ensure engineering practicability.
The segmented unit influence function method is adopted for roll deformation calculation. It balances calculation accuracy and efficiency. De plus, it avoids the low precision of analytical methods and the non-convergence problem of finite element simulation for thin strips. Under asymmetric working conditions, the entire roll body is analyzed based on the Castigliano’s theorem.
The variational method is used for strip plastic deformation calculation to adapt to the three-dimensional deformation characteristics of cold-rolled strips. A multi-cycle iterative algorithm is constructed to revise inter-roll pressure, force de roulement, exit thickness and tension. The system introduces transverse metal flow and uses cubic spline fitting to simulate transverse thickness distribution. Enfin, le système de calcul optimisé prédit avec précision la répartition de la pression, épaisseur de sortie et variation de la tension transversale sous différentes forces de flexion asymétriques.
## 4. Avantages techniques et effets d'application du contrôle asymétrique du pliage des rouleaux de travail
### 4.1 Optimisez la pression entre les rouleaux et prolongez la durée de vie des rouleaux
Le contrôle asymétrique du pliage des rouleaux de travail équilibre efficacement la pression de contact entre les rouleaux de travail, rouleaux intermédiaires et rouleaux de secours. Il réduit la pression maximale aux extrémités des rouleaux et améliore la répartition inégale de la pression.. La technologie soulage l’usure asymétrique des rouleaux et évite le pelage de la surface du rouleau, réduisant ainsi les coûts de maintenance des équipements et les taux de défaillance.
### 4.2 Élimine l'épaisseur asymétrique et l'écart de tension
Les bandes entrantes avec une épaisseur de coin provoquent toujours une tension transversale déséquilibrée et des vagues sur un seul bord. Symmetric bending cannot solve one-sided thickness difference. Cependant, asymmetric work roll bending control corrects transverse thickness deviation and realizes uniform tension distribution at the strip exit. It fundamentally eliminates asymmetric shape defects.
### 4.3 Replace Roll Tilting for High-Precision Fine Adjustment
Using Bessel standard deviation as the evaluation index, practical comparison shows that small roll tilting adjustments cause large standard deviation fluctuation and poor shape stability. When users replace tilting with asymmetric work roll bending control, shape deviation and fluctuation range drop significantly. It greatly improves strip uniformity and overall control accuracy under minor asymmetric defects.
## 5. Technical Summary
Asymmetric work roll bending control breaks the limitation of traditional symmetric bending. It forms a complete theoretical and practical system for asymmetric strip shape correction. The technology optimizes roll stress distribution, reduces roller wear and lowers production risks. It replaces unstable roll tilting in fine adjustment scenarios and achieves high-precision shape control with low renovation cost.
Compatible with HC, UC, CVC and conventional four-high cold rolling mills, asymmetric work roll bending control features simple logic and low application thresholds. It has become a key practical technology for eliminating asymmetric strip defects and meeting high-end cold rolling production requirements.